■ Thermal Management Materials Cannot Be Used as They Are
Many materials supplied by material manufacturers come in forms such as
sheets,
rolls,
films,
and foils.
But inside actual products, there are
ICs,
connectors,
screws,
sensors,
wiring,
and steps.
That is why a simple rectangle often does not fit.
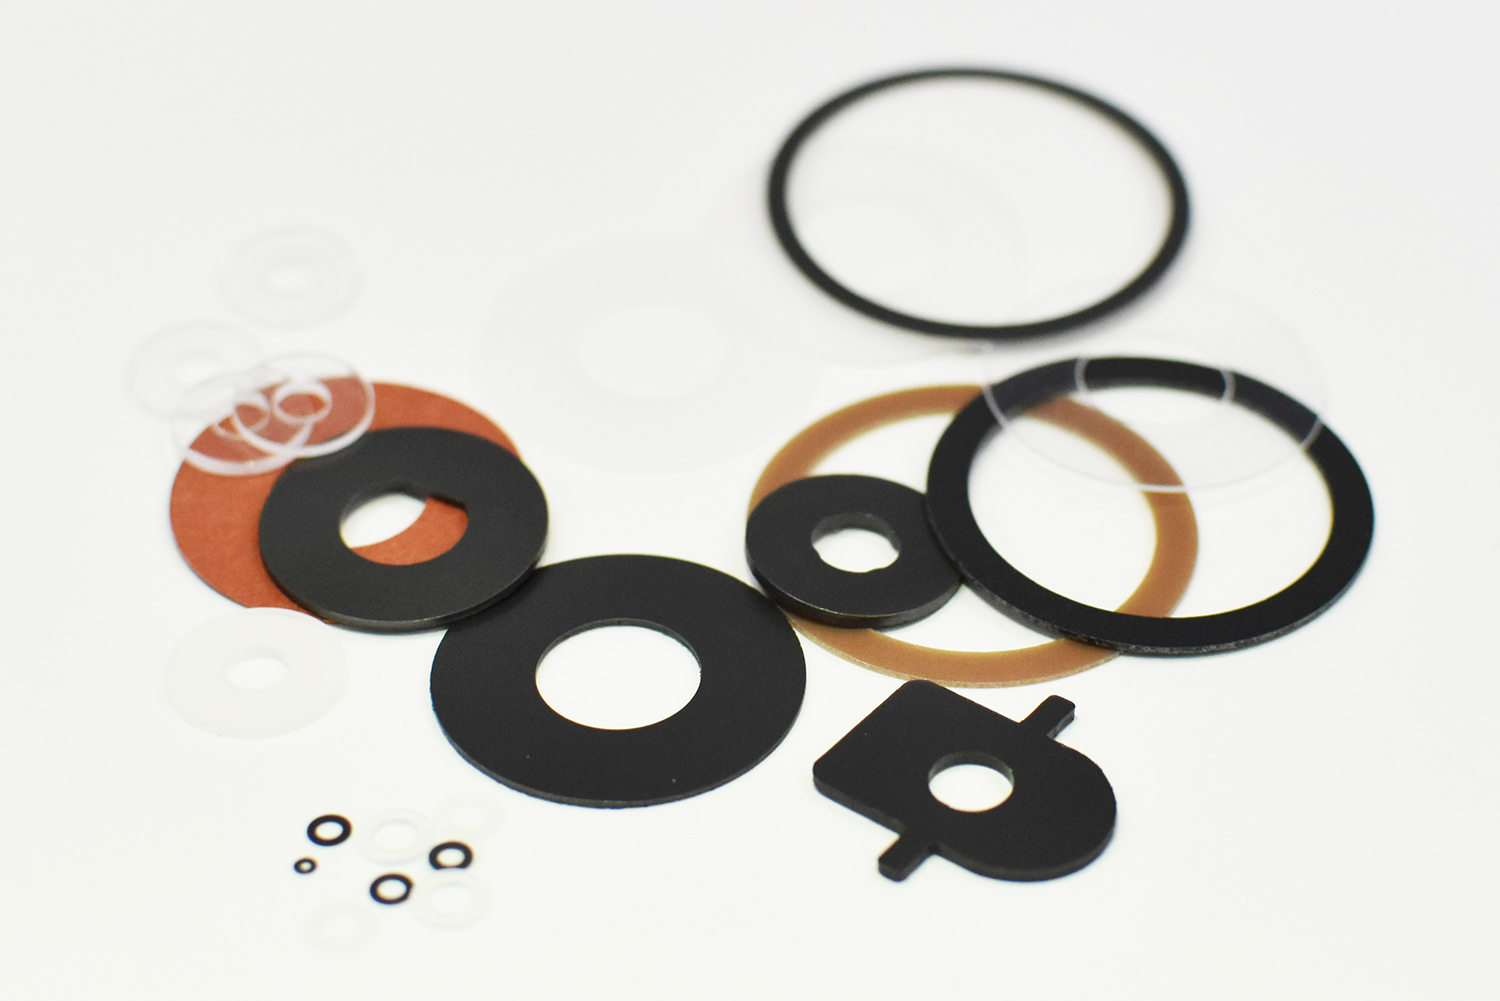
What is needed is processing such as
making holes,
avoiding certain parts,
matching the outer shape,
creating narrow sections,
and combining multiple parts into one sheet.
In other words, processing is the process that connects materials and product design.
■ Why Is High Precision Needed for Thermal Management?
Heat is invisible.
That is why it is sometimes thought that
“it’s no problem if the TIM shifts a little.”
But in reality, a deviation of a few mm, or in some cases even less, can affect thermal performance.
For example, TIM is applied on top of a heat-generating component.
The TIM shifts slightly.
Part of the heat-generating area comes off the TIM.
Then heat cannot be transferred sufficiently in that part.
In other words, a deviation in component position becomes a deviation in the heat path as is.
■ In Thermal Management, "Area" Is Performance
TIM connects the heat source and the heat dissipation component.
That is why contact area is important.
For example, for a 10 mm square heat-generating component, the TIM is also designed at 10 mm square.
The TIM shifts by 1 mm.
Then a non-contact area appears along one side.
In small components, even a slight deviation becomes a large proportion of the contact area.
In other words, the smaller the component, the larger the impact of the same 1 mm deviation.
■ With Miniaturization, the Meaning of Processing Accuracy Changes
A 0.1 mm deviation on a 100 mm component.
A 0.1 mm deviation on a 5 mm component.
The absolute value is the same.
But the relative impact is very different.
The more
semiconductors,
sensors,
optical components,
and wearables
are miniaturized, the more important processing accuracy becomes.
In other words, miniaturization of products tightens the requirements for processing accuracy.
■ Outer Shape Accuracy Alone Is Not Enough
When people hear high-precision die-cutting, it is easy to imagine
outer dimensions ±○ mm.
But for thermal management components, that is not all.
What matters is
the outer shape,
hole positions,
opening positions,
positions between components,
lamination positions,
and adhesive positions.
For example, even if the outer dimensions are correct, if the central opening is off, it will cover the necessary part.
In other words, both dimensional accuracy and positional accuracy are needed.
■ Why Hole Positions Matter
Thermal management components sometimes have holes to avoid screws and connectors.
If these hole positions are off, problems occur such as
it cannot be assembled,
it interferes with screws,
the component lifts,
or it is forced in.
Then even the TIM contact state may change.
In other words, hole processing, which at first glance seems unrelated to heat, ultimately connects to thermal performance.
■ Opening Shapes Also Have Meaning
Only part of an insulating film is opened.
TIM is brought into contact through that part.
Or
only the sensor area is avoided.
Only the antenna area is avoided.
In such designs, the opening position becomes important.
If the opening is too large, the insulated area decreases.
If too small, it obstructs the heat path.
In other words, in high-precision processing, what matters is not “cutting” but “differentiating where functions remain and where they are removed.”
■ Creating Where Heat Flows and Where It Does Not Through Shape
In thermal management, making the entire surface thermally conductive is not always right.
For example,
we want to release heat from the central heat-generating part.
We do not want to transfer heat to the surrounding temperature sensor.
We do not want heat to spread toward the battery.
This can happen.
In that case, the heat path is created through
the shape of the thermally conductive material,
openings,
slits,
and placement.
In other words, the processed shape itself becomes an element that designs the flow of heat.
■ Shape Is Especially Important for Graphite
Graphite sheets excel at spreading heat in the in-plane direction.
But in which direction and how far heat spreads changes with shape.
Extending it long and narrow from the heat-generating part toward the enclosure.
Avoiding surrounding components.
Widening only where needed.
Through such processing, the material’s heat-spreading performance is used inside the product.
In other words, cutting graphite is also creating a path for heat.
■ The Longer and Narrower the Shape, the Harder the Processing
To release heat laterally, graphite and metal foil are sometimes designed long and narrow.
But the longer and narrower they get, the more problems arise:
they deform,
break,
shift,
and are hard to transport.
Furthermore, in volume production, that shape must be made the same way tens of thousands of times.
In other words, high-precision processing requires not only dimensional accuracy, but also the technology to process without breaking the shape.
■ With Metal Foil, Burrs Become a Problem
When copper foil or aluminum foil is die-cut, burrs can form on the edges.
Even very small burrs can lead to problems such as
damaging insulating films,
contacting adjacent components,
and becoming foreign matter.
Especially in high-voltage applications, small metal protrusions affect insulation reliability.
In other words, in metal foil processing, not only outer dimensions but edge quality itself becomes a product function.
■ As Films Get Thinner, Damage During Processing Can No Longer Be Ignored
If the material is thick, it can withstand some processing stress.
But with thin films, problems such as
stretching,
wrinkling,
tearing,
and deformation
become more likely.
For example, a film of tens of μm is processed with high precision.
Even if only the dimensions are matched, if the material is wavy, it may lift during assembly.
In other words, in thin-film processing, quality includes shape stability after cutting.
■ Soft TIM Is Not "Done Once It Is Cut"
Some TIMs are very soft materials.
Being soft is advantageous for conforming to steps and for contact.
But it makes processing difficult.
The blade presses.
The material deforms.
It is cut in that state.
The blade is released.
The material springs back.
Then the dimensions may differ between during and after processing.
In other words, with soft materials, the finished dimensions sometimes cannot be determined by die dimensions alone.
■ With Adhesives, the Behavior of the Adhesive Itself Must Also Be Considered
When adhesives are die-cut, problems can occur such as
adhesive sticking to the blade,
adhesive oozing from the edges,
and adhesive stringing.
If this continues,
processing accuracy changes,
foreign matter increases,
and material sticks to the die.
In other words, in adhesive processing, it is necessary to consider even the interaction between the blade and the adhesive.
■ Each Material "Cuts" Differently
PET film.
PI film.
Foam.
Copper foil.
Aluminum foil.
Graphite.
TIM.
Adhesive.
These cannot all be processed the same way with the same die.
Hardness,
elongation,
brittleness,
tackiness,
thickness,
and laminate composition
differ.
In other words, in high-precision die-cutting, it is important to create processing conditions matched to material properties.
■ Die Accuracy Alone Does Not Make High-Precision Processing
A high-precision die is made.
That alone does not necessarily produce high-precision parts.
In practice,
material tension,
feed accuracy,
die clearance,
processing speed,
temperature and humidity,
and material lot
all have an effect.
In other words, high-precision processing is established by a high-precision die + a stable process.
■ In Reel Processing, Feed Accuracy Is Important
Roll material is processed while being fed a fixed amount at a time.
Even if each feed error is small, repetition leads to positional deviation.
Especially in
multi-step processing,
multiple die-cuts,
and post-lamination processing,
the positions of earlier and later processes must be aligned.
In other words, in long-run processing, feeding material accurately is itself a processing technology.
■ If Tension Changes, Dimensions Also Change
A thin film is pulled strongly.
It stretches slightly.
It is die-cut in that state.
The tension is released.
The material springs back.
Then dimensions that were correct during processing may change after completion.
In other words, in thin-film and long-run processing, tension control becomes dimensional control.
■ In Multiple Processes, How to Hold the Reference Position Matters
Holes are processed in the first step.
Another material is laminated in the second step.
The outer shape is cut in the third step.
If each process deviates independently, the final positional deviation becomes large.
That is why position is controlled using
reference holes,
recognition marks,
and feed pitch.
In other words, in multi-step processing, what to use as the reference for aligning everything is important.
■ High-Precision Processing Goes Hand in Hand with Lamination Accuracy
Thermal management components do not necessarily involve processing just one material.
For example,
Graphite + Insulating film + Adhesive
are laminated.
If each material deviates by ±0.1 mm, the functional position in the final component may change significantly.
In other words, both
die-cutting accuracy
and lamination accuracy
are needed.
■ Processing Tolerances Stack Up
Outer shape ±0.1 mm.
Lamination ±0.1 mm.
Application ±0.2 mm.
Each looks like a small number on its own.
But in the final product, they stack up.
In other words, working backward from the final positional accuracy the customer needs, it is necessary to consider how much tolerance to allocate to each process.
■ Summary of Part 1: Processing Accuracy Becomes the Accuracy of the Heat Path as Is
Heat is invisible.
That is why it is easy to think “it’s no problem if it shifts a little.”
But in reality,
if the TIM shifts by 1 mm, the contact area decreases by that much.
If hole positions are off, the component lifts.
If burrs remain, they damage the insulating film.
If opening positions are off, they block the heat path itself.
The smaller the component, the greater the meaning of the same 0.1 mm.
And accuracy is not determined by the die alone.
Each material cuts differently.
Soft TIM springs back when the blade is released.
Thin films become wavy after processing.
Adhesives leave residue on the blade.
If tension changes, dimensions also change.
With multiple processes, where to place the reference is called into question.
Furthermore, each tolerance stacks up in the final product.
In other words,
high-precision processing is established by both a high-precision die and a stable process.
Then how strict should accuracy be?
In Part 2, we consider this.
Column Supervisor: Koji Kakumoto (President, OTIS Co., Ltd.)
After studying abroad and working in planning and development at a trading company, he joined OTIS Co., Ltd. in 2011. While primarily working in the Corporate Planning Department, he has also served concurrently in manufacturing and technical divisions, and since 2018 has served as President, working to drive business growth and strengthen the organization.
This article is a general technical explanation intended for educational purposes and does not refer to any specific company, product, or technology.