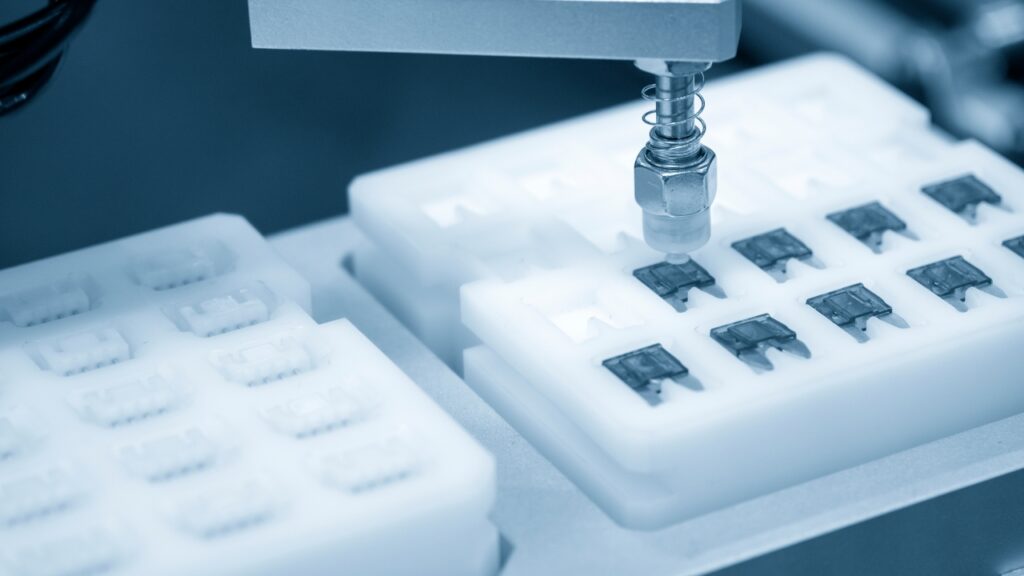
■ Check Equipment Specifications at an Early Stage
If, right before volume production,
it cannot be picked up by suction,
the winding direction is reversed,
or the carrier width does not fit the equipment,
the rework is large.
That is why from the prototyping stage,
equipment specifications,
whether it will be automated in the future,
and the required takt time
are confirmed.
In other words, it is important
not to leave volume production equipment for later.
■ Working Back from Takt Time
At 10 seconds per unit
and a few hundred units a day,
manual work may be fine.
At 1 second per unit
and several million units a year,
automation is needed.
In other words, whether to convert to reels is decided
not only by component performance, but by
quantity and takt time.
■ Not Everything Needs to Be Converted to Reels
If the quantity is small,
the component is very large,
or the process benefit of reel conversion is small,
loose parts or tray supply may be better.
In other words, what matters is
not reel conversion itself.
It is choosing the supply format best suited to the customer’s process.
■ Tray Supply Can Also Be Suitable
With
large components,
components prone to warping,
and thick laminated components,
winding on a reel may change the shape.
In that case,
they are arranged in a fixed posture on a tray.
This is also a supply format for automation.
In other words, automation support
is not limited to reels.
■ The Strength of Reel Supply Is Continuity
Reels can
supply for long periods without stopping.
Components can be fed
at a fixed pitch
and in a fixed posture.
That is why they work well with high-speed automatic machines.
In other words, the value is especially high for
mass production,
small components,
and thin-film components.
■ Reel Length Also Affects Productivity
100 units per reel.
The equipment changeover frequency is high.
10,000 units per reel.
Long operation is possible.
But the reel becomes large.
Winding pressure is applied to the material.
In other words, reel length must also be decided by balancing
equipment uptime,
logistics,
and material properties.
■ Splice Management Is Also Important
With long materials, the original roll sometimes has splices.
Material changes are also needed during reel processing.
The equipment mistakes the splice for a product.
Or it catches during transport.
That is why
splice positions
and identification methods
must be managed.
In other words, with long-run supply,
information other than the product also needs to be conveyed to the equipment.
■ Reel Winding Direction Becomes a Specification
Adhesive side inward.
Outward.
The direction of the component’s leading end.
Just a difference in these can keep it from fitting the customer’s equipment.
In other words, for reel products,
winding direction
and face direction
become official product specifications.
■ Warping Changes with Winding Diameter
Small-diameter reel.
Compact.
But a strong bending set on the component.
Large-diameter reel.
Small bending set.
But the logistics size is large.
This is especially important for graphite and metal foil laminates.
In other words,
reel design is also component flatness design.
■ Winding Pressure Is Also Controlled
Wound tightly.
The reel is stable.
But soft TIM is compressed.
Adhesive squeezes out.
Wound loosely.
It shifts inside the reel.
In other words, appropriate winding pressure is needed.
■ Reel Posture During Storage Is Also Important
Laid flat.
Stood upright.
High-temperature storage.
Long-term storage.
Depending on these,
material compression
and winding shift
can occur.
In other words, for reel products, even storage conditions after processing become quality conditions.
■ Components Must Not Move with Transport Vibration
At shipment.
Pitch normal.
On arrival at the customer.
Components have moved slightly on the liner.
This affects equipment recognition.
That is why it is necessary to consider transport too, including
adhesive holding force,
winding state,
and packaging.
■ Also Consider High Temperatures in Summer Transport
Temperatures inside trucks and containers rise.
The adhesive softens.
Peel force changes.
Components may
shift.
In other words, components for automation must be
usable on equipment not only inside the factory, but after going through the logistics environment.
■ Being Usable on the Customer's Equipment from the Start Is Important
It arrives at the customer.
The reel is set on the equipment.
It can be used with almost no condition adjustment.
This is ideal.
If equipment conditions must be changed for every lot, productivity is poor.
In other words, there is value in the processing manufacturer stabilizing
pitch,
peeling,
and position.
■ Reducing Equipment Stoppage Rates Becomes Component Value
The material unit price per sheet is lowered by 1 yen.
1 million yen saved per year.
But equipment stops frequently due to component peeling defects.
People restore it.
If production losses are 5 million yen per year,
it is not a cheap component.
In other words, for components for automation,
value must be considered including equipment uptime.
■ Shifting the Perspective from "Unit Price" to "Process Cost"
Reel conversion adds
carriers,
liners,
and processing steps.
The component unit price may go up.
But if on the customer side,
operator reduction,
improved equipment takt,
improved positional accuracy,
and defect reduction
are possible, the total cost goes down.
In other words,
do not judge the value of reel conversion by component price alone.
■ Combining Part Count Reduction and Automation
TIM,
insulating film,
and graphite
are applied three times.
The equipment also has three processes.
They are laminated in irregular shapes in advance.
Converted to reels as an integrated component.
The customer applies once.
Then
equipment processes,
recognition counts,
and application errors
may be reduced.
In other words, lamination + reel conversion further increases the value of automation.
■ The More Composite the Component, the Greater the Effect of Reducing Customer Processes
Reel conversion of a single component.
One process is automated.
Integrating multiple functional materials and converting to reels.
Multiple processes become one.
In other words, the more combining is done on the processing manufacturer’s side,
the more the customer’s process may be changed significantly.
■ However, Integrating Too Much Raises the Component Price
Materials increase.
Processing increases.
The loss from a single defect is also large.
That is why
the process reduction savings from integration
and the increase in component price
are compared.
In other words, in automation proposals, it is necessary to look at the economics of the customer’s entire process.
■ The Value of Supplying as Inspected Reels
Processing.
Image inspection.
Only good parts are converted to reels.
Supplied to the customer’s equipment.
This may reduce the process of checking component appearance on the customer’s side.
In other words, reel products have value not as mere processed products,
but as inspected volume production inputs.
■ Leave NG Parts in the Reel or Remove Them?
Defects are detected by image inspection.
The position is communicated to the equipment.
Or defective parts are removed so only good parts are lined up.
There are several methods.
They must match the customer’s equipment specifications.
In other words, inspection and supply format are also considered together.
■ Summary of Part 2: Reel Conversion Is Not the Goal but a Means
Reel supply is a powerful method.
Fixed pitch. Fixed orientation. Fixed position.
It works well with high-speed automatic machines.
However, not everything should be converted to reels.
If the quantity is small, manual work may be viable.
Large components and components prone to warping change shape when wound.
Tray supply may be better.
In other words, what decides it is not component performance.
It is quantity, takt time, and the customer’s process.
And even after deciding on reels, design continues.
If the winding diameter is small, a bending set remains.
Winding tightly compresses TIM and makes adhesive squeeze out.
Making it longer makes the equipment less likely to stop, but the reel becomes larger.
If the winding direction is wrong, it does not even fit the equipment.
Furthermore, components change even after leaving the factory.
Adhesive softens in high-temperature logistics.
Transport vibration moves components on the liner.
Even if there is no problem in pre-shipment testing, it does not peel on the customer’s equipment.
In other words,
what is required of components for automation is
not working inside the factory, but working on the customer’s equipment after going through logistics.
And the way of looking at value also changes.
Even if lowering the material unit price by 1 yen saves 1 million yen a year,
if 5 million yen a year is lost to equipment stoppages from peeling defects, it is not a cheap component.
Reel conversion adds carriers, liners and processing, raising the component unit price.
Even so, if it reduces operators, raises takt and reduces defects,
the customer’s total cost goes down.
In other words,
judge by process cost, not component unit price.
Then how can that supply be maintained for tens of thousands of units?
In Part 3, we move on to keeping promises in volume production.
Column Supervisor: Koji Kakumoto (President, OTIS Co., Ltd.)
After studying abroad and working in planning and development at a trading company, he joined OTIS Co., Ltd. in 2011. While primarily working in the Corporate Planning Department, he has also served concurrently in manufacturing and technical divisions, and since 2018 has served as President, working to drive business growth and strengthen the organization.
This article is a general technical explanation intended for educational purposes and does not refer to any specific company, product, or technology.